ABOUT US
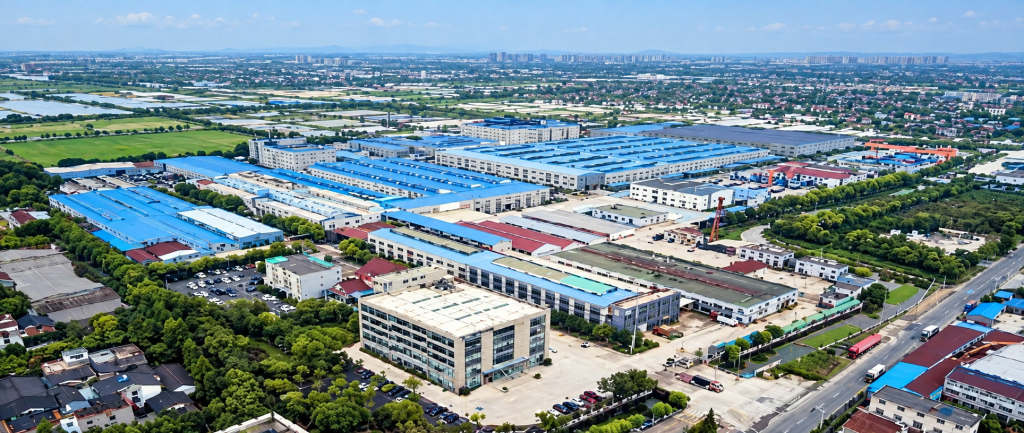
Hubei Zhejian Transmission Technology Co., Ltd
The company specializes in the production of “Double Arrow” brand rubber conveyor belts and has an annual production capacity of more than 90 million square meters of various types of rubber conveyor belts. It has established a comprehensive innovation management system and has obtained certifications for the ISO 9001 Quality Management System, ISO 14001 Environmental Management System, OHSAS 18001 Occupational Health and Safety Management System, and ISO 50001 Energy Management System, as well as certifications for its measurement management system and national standardization good-practice enterprise status. Its products are widely used in industries such as mining, metallurgy, coal, transportation, building materials, electric power, chemicals, light industry, and grain processing.
The company enjoys a strong reputation within the industry. It serves as a Vice Chairman Member of the China Rubber Industry Association and is one of the principal organizations involved in drafting national and industry standards for conveyor belt products. For twelve consecutive years, it has ranked first among the Top 10 enterprises in China’s conveyor belt industry. The company has also obtained both international and domestic certifications under the “Made in Zhejiang” program and was among the first group of Industrial Enterprise Brand Cultivation Demonstration Enterprises recognized by China’s Ministry of Industry and Information Technology.
Hubei Zhejian Transmission Technology Co., Ltd. was established in 1986 and is located in Tongxiang City, in the heart of the Yangtze River Delta. It is a high-tech enterprise specializing in the production of rubber conveyor belts and the design and provision of material-handling system solutions and services.
The company was listed on the Shenzhen Stock Exchange in April 2010, becoming the first company in the industry and the first enterprise in Tongxiang City to be listed on the Main Board.
The company ranks among the top three globally in the conveyor belt industry in terms of overall strength, while its single-factory production capacity ranks first in the world. It is a leading enterprise in China’s rubber conveyor belt industry and has been recognized as a National Manufacturing Single Champion Enterprise. It has also ranked No. 1 in China’s conveyor belt industry for 14 consecutive years based on comprehensive industry rankings.
The company serves as a Vice Chairman Member of the China Rubber Industry Association and is one of the principal organizations involved in drafting international, national, and industry standards for conveyor belts.
Hubei Zhejiang Transmission Technology Co., Ltd. has successfully passed the inspection and certification procedures of global industry leaders such as Rio Tinto and BHP, becoming an approved supplier. The company has also been included on the list of strategic partners of leading global mining companies, including Rio Tinto, BHP, and Vale.
Core Strengths: Expert in Long-Distance, Environmentally Friendly, Energy-Efficient and High-Efficiency Material Conveying System Solutions
The company ranks among the top three globally in the conveyor belt industry in terms of overall strength, while its single-factory production capacity ranks first in the world. It is a leading enterprise in China’s rubber conveyor belt industry and has ranked No. 1 in China’s conveyor belt industry for 13 consecutive years. It was also the first company in the industry to be listed on the Main Board.
The company’s long-distance, environmentally friendly, high-efficiency and energy-saving conveyor belts have received distinctions such as the “Great World Guinness Record” and have been acclaimed as an “Aerial Transportation Corridor.”
Key Characteristics: Focused, Research-Driven, Professional
Founded in 1986, the company has devoted 38 years to research and development in the field of material conveying system solutions. Its capabilities are supported by a 6,000-square-meter provincial-level enterprise research institute, more than 260 technical professionals, 53 production lines, and an annual production capacity of 90 million square meters.
These resources have established the company’s strengths in specialization, dedicated research, and professional expertise, while reinforcing its role as one of the principal organizations responsible for drafting international, national, and industry standards for conveyor belts.
The Company operates a 6,000-square-meter provincial-level enterprise research institute. In June 2017, it was recognized as the Energy-Saving and Environmentally Friendly Conveyor Belt Technology Center of China’s Rubber Industry. The Company has also established a provincial-level postdoctoral research workstation in cooperation with Zhejiang University and carries out industry-university-research collaboration with institutions including Qingdao University of Science and Technology, Taiyuan University of Science and Technology, Zhejiang Sci-Tech University, and Northeastern University. It is also recognized as a Provincial International Science and Technology Cooperation Base.
The Company is equipped with a world-leading low rolling resistance testing system and a dynamic splice fatigue testing machine designed by CDI of the United States, together with a range of advanced inspection and testing instruments. At present, only three such dynamic splice fatigue testing machines exist worldwide, with the other two located at Leibniz University Hannover in Germany and the University of Newcastle in Australia. The machine owned by the Company offers the most comprehensive testing capabilities and the highest force capacity, enabling testing up to ST15000.
The Company currently has more than 260 R&D personnel, including one expert receiving a Special Government Allowance from the State Council, nine professor-level senior engineers, and four members of the National Conveyor Belt Expert Group. More than 50% of its technical personnel hold intermediate-level or higher professional qualifications. The Company has undertaken one national key scientific research project and two provincial key science and technology projects, and has developed 21 provincial-level new products. It holds 116 authorized invention and utility model patents, including one international patent, and has taken the lead in drafting 39 international, national, and industry standards, including two international standards.
The Company has a total of 81 vulcanization production lines, including those under construction at Taisheng Intelligent Conveyor Belt Technology Co., Ltd. These comprise 20 steel-cord conveyor belt lines, 47 fabric-carcass conveyor belt lines, 3 solid-woven belt lines, 5 drum-vulcanization lines, 4 special-purpose belt lines, and 2 patterned belt lines.
According to the Company’s plan, by 2024 its annual production capacity was expected to reach 150 million square meters. Its production capabilities include conveyor belts with a maximum width of 3,000 mm, steel-cord conveyor belts with strength ratings up to ST10000, aramid conveyor belts up to DPP3150, and PVC/PVG conveyor belts with a maximum width of 1,800 mm and strength ratings up to 2500S. These capabilities provide a solid foundation for the Company’s goal of becoming a world-class conveyor system service provider.
The Company has established a complete industrial chain covering rubber cultivation and processing, including a natural rubber experimental base; conveyor belt manufacturing; sales and installation; and the design and servicing of material conveying system solutions. In 2015, it also expanded into the healthcare and elderly-care industry.
Address: Room 1, Floor 30, Building 5, No. 5, 7, 9, Youyi Road, Jianghan District, Wuhan City, Hubei Province
E-mail: hubeizhejiantransmissiontech@gmail.com